Sep 28, 2026Quality Inspection Guides
Product Inspection Checklist for China Orders | G&D
Learn how to build a practical product inspection checklist for China orders, covering requirements, references, check methods, sample quantities, acceptance criteria and evidence.
How to Build a Product Inspection Checklist for a China Order
Most buyers already have the information needed for an inspection checklist. It may be spread across a purchase order, product specification, technical drawing, approved sample, artwork file, packing instruction and email conversation.
The problem is that these documents were not necessarily written as instructions for an inspector working at the factory.
“Check the zipper,” “color as approved” and “strong export carton” express expectations, but they do not explain how to perform the check, how many units to examine, what result is acceptable or what evidence should appear in the report.
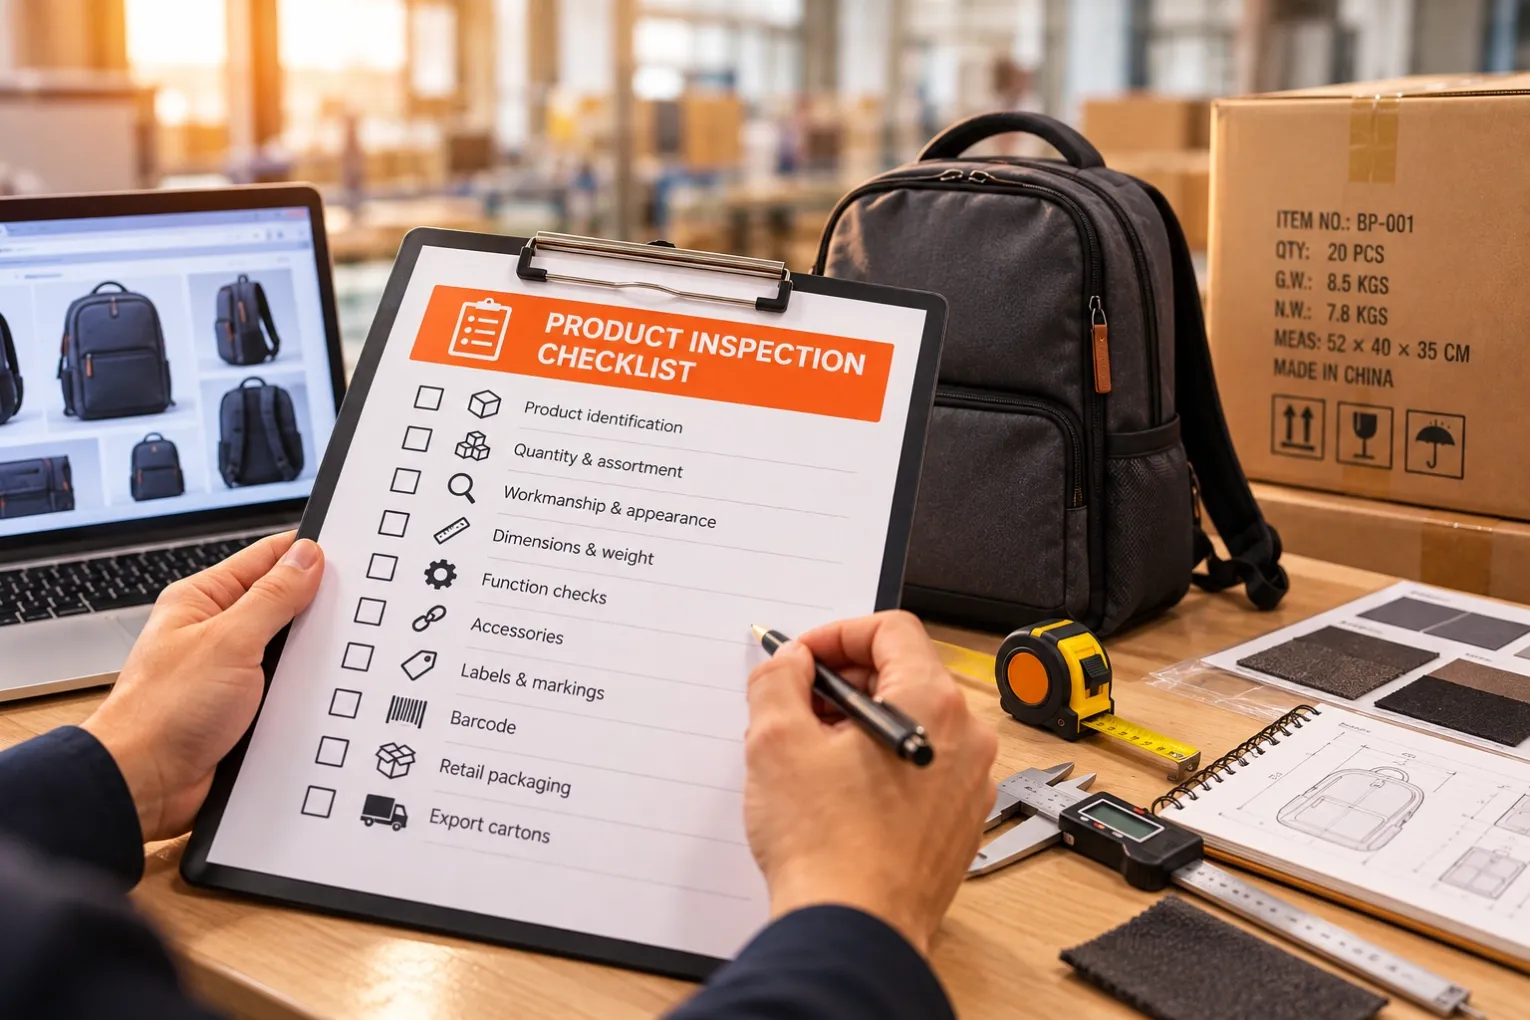
A product inspection checklist should identify the product and order, state each measurable requirement, name the approved reference, explain the inspection method, define how many units are checked, set the acceptance criteria, and specify the evidence to record. It should also cover workmanship, function, labels, packaging and buyer-defined risks relevant to that product.
What Should a Product Inspection Checklist Include?
A useful checklist begins with product and order identification. The inspector should be able to confirm the purchase order, model, SKU, color, size, order quantity and packaging configuration before checking quality.
The remaining checkpoints depend on the product. They may cover:
- quantity and assortment;
- workmanship and appearance;
- dimensions and weight;
- observable materials and components;
- construction and assembly;
- function and product-specific tests;
- accessories, manuals and inserts;
- artwork, printing and logos;
- product labels, markings and barcodes;
- retail packaging and export cartons;
- buyer-specified critical points.
Not every category belongs in every checklist. A rain jacket needs waterproof-related checks, while a chair needs stability and assembly checks. Adding irrelevant items makes the document longer without making the inspection better.
A checklist must also distinguish between what can be checked on site and what requires another form of verification. An inspector may confirm visible construction, component markings or supplied accessories. Hidden material composition or chemical properties may require independent laboratory testing.
The Six Fields Behind a Usable Product Inspection Checklist
Every important checkpoint should answer six questions:
Requirement → Reference → Inspection Method → Check Quantity → Acceptance Criteria → Evidence
1. Requirement
The requirement states what the finished product must achieve.
It may be a dimension, material, function, construction detail, appearance standard, packaging configuration or labeling requirement. Write the actual requirement instead of an instruction such as “check size.”
Example:
Product width must be 500 mm ± 3 mm.
2. Reference
The reference tells the inspector where the requirement comes from.
It may be the latest product specification, technical drawing, approved physical sample, approved color swatch, artwork file, packaging drawing, purchase order or buyer comment.
Use revision numbers or dates where possible. “Approved artwork” is unclear if three artwork files have been exchanged and the factory is using an older version.
3. Inspection Method
The method explains what the inspector should do.
For the 500 mm width requirement, the method could be:
Place the product flat without stretching and measure the defined position using suitable measuring equipment.
A method matters because two people can interpret “check width” differently. One may measure the outer edge, another the internal opening, and a third may measure while the product is folded.
4. Check Quantity
The checklist should state how extensively each checkpoint is applied.
The quantity might be:
- all units in the workmanship sample;
- a defined number of units per SKU;
- the agreed AQL sample;
- a smaller quantity under a special inspection level;
- one carton from each selected packing group;
- a buyer-specified number;
- a limited quantity for a destructive test.
The same quantity does not have to apply to every checkpoint.
5. Acceptance Criteria
Acceptance criteria define what result is acceptable.
For the width example, the criterion is:
Each measured result must be between 497 mm and 503 mm.
Some criteria are objective, such as a dimension, weight or component count. Others require comparison with an approved reference. Cosmetic acceptance may depend on visibility, location, severity and agreed defect classification rather than a universal numerical tolerance.
6. Evidence
Evidence tells the inspector what to record for the buyer.
For the width check, the report may need a measurement table showing each result and representative photographs of the measuring position.
Without an evidence requirement, a report may only say “Pass.” That does not show what was measured, which samples were checked or how close the results were to the limit.
How to Turn Product Specifications Into Inspection Checkpoints
A specification describes the product. A checkpoint explains how to verify it.
The difference is easiest to see in practical examples:
Weak Requirement | Usable Inspection Checkpoint |
|---|---|
Good zipper | Open and close the zipper through its full travel for the agreed number of cycles on the specified sample quantity. Check for jamming, separation, missing teeth and slider failure. |
Correct color | Compare the product with the approved physical color reference under the agreed viewing conditions. Record any visible shade difference within one product or between sampled units. |
Printing should be good | Compare the logo with the approved artwork for content, orientation, position and color. Check for visible smearing, missing print and unacceptable registration. |
All accessories included | Open the agreed sample quantity and compare every accessory and its quantity with the approved component list. Record missing, wrong or extra items. |
Strong carton | Confirm the specified carton construction and closure method, then perform the agreed packaging check or test using the defined procedure and quantity. Record carton and product condition afterward. |
The checkpoint does not need to be complicated. It needs to be repeatable. Another inspector should be able to read it and perform substantially the same check.
How Should Approved Samples Be Used?
An approved sample can be a useful reference for appearance, color, workmanship, construction, component placement and packaging presentation.
It is less effective for details that can be defined objectively. If the product width must be 500 mm ± 3 mm, the checklist should state that tolerance. “Same as approved sample” forces the inspector to measure the sample, assume that measurement is intentional and decide how much variation is acceptable.
The sample should also be clearly identified. The checklist can record the sample version, approval date, location and any approved changes made after the sample was produced.
The approved sample is therefore one reference within the checklist, not the whole checklist. How to Make Sure Bulk Production Matches the Approved Sample explains how that reference can be controlled throughout production.
For a newly developed product, reviewing the reference before production starts can also expose missing dimensions, unclear accessories or outdated artwork. A Pre-Production Sample Review can be useful when the final production standard still contains open questions.
How Should Sample Quantities Be Defined?
Workmanship defects are often evaluated across a larger random sample. Measurements, function checks and time-consuming or destructive tests may use smaller quantities agreed before the visit.
For example, an inspection might include:
- workmanship checks on the full AQL sample;
- measurements on five units per size;
- a zipper operation check on five units per SKU;
- barcode scanning on three units per barcode;
- one carton drop test;
- an accessory check on all sampled sellable units.
These are examples, not universal quantities. The correct quantity depends on the product, the test, the number of SKUs and the buyer’s requirements.
As ASQ explains, an acceptance sampling plan defines sample sizes and the associated acceptance or non-acceptance criteria. It does not automatically define the quantity for every measurement or functional test in an inspection checklist.
For a practical explanation of how the main inspection sample is calculated, see How Many Pieces Are Inspected During a Quality Inspection?.
What Evidence Should the Inspector Record?
A checklist should define not only what to check, but what the buyer expects to see afterward.
Depending on the checkpoint, useful evidence may include:
- actual measurement results;
- defect descriptions and close-up photographs;
- product and component photographs;
- label and marking photographs;
- decoded barcode values;
- function-test results;
- photographs before, during and after a test;
- accessory counts;
- carton dimensions, weights and condition;
- quantity observations;
- remarks about unavailable references or testing limitations.
The evidence should answer the buyer’s next question. If a barcode was scanned, record the decoded value. If a product failed a function test, show the sample, test condition and observed failure. If a dimension was outside tolerance, report the actual measurement rather than only “Not Conform.”
Example Product Inspection Checklist
The following is a simplified hypothetical example for a backpack. The quantities and criteria are only examples; they are not universal backpack requirements.
Checkpoint | Requirement | Reference | Method | Check Quantity | Acceptance Criteria | Evidence |
|---|---|---|---|---|---|---|
Product identity | Correct model, color and size | PO and SKU list | Compare product and labels with order details | All sampled units | No wrong model, color or size | Product and label photos |
Finished width | 300 mm ± 5 mm | Drawing Rev. B | Lay flat and measure the defined position | 5 units per SKU | 295–305 mm | Measurement table and photos |
Main zipper | Complete 10 full cycles | Buyer test instruction | Open and close through full travel | 5 units per SKU | No jamming, separation, missing teeth or slider failure | Test result and failure photos |
Shoulder strap | Withstand agreed load and duration | Product specification | Apply the specified load using the agreed setup | 1 unit per SKU | No tearing, stitch failure or strap separation | Setup, load and result photos |
Accessories | One rain cover and one instruction card | Approved component list | Open the retail pack and count components | All sampled units | Correct items and quantities in every checked pack | Accessory layout photo |
Logo printing | Correct artwork, position and orientation | Artwork Rev. 4 | Compare visible print with approved file | All sampled units | No wrong artwork, smearing, missing print or reversed orientation | Representative and defect photos |
Barcode | Correct EAN for each SKU | Approved barcode list | Scan and compare decoded value | 3 units per SKU | Decoded value matches the assigned SKU | Scan result and label photo |
Export carton | Correct quantity and carton mark | Packing specification | Open selected cartons and compare contents and marks | Selected cartons | Correct SKU, case quantity, carton number and mark | Carton and contents photos |
A real checklist may contain more detail, but every row should still answer the same six questions.
Common Product Inspection Checklist Mistakes
The most common problems are not missing pages. They are unclear instructions.
- Copying the purchase order without converting specifications into checks.
- Using words such as “good,” “normal,” “strong” or “acceptable” without defining them.
- Listing a target dimension without a tolerance.
- Referring to an approved sample that is not available or clearly identified.
- Using outdated drawings, artwork or packaging files.
- Giving a test name without its method, equipment, duration or load.
- Applying one sample quantity to every type of check.
- Omitting retail packaging, export cartons, labels or barcodes.
- Treating every cosmetic issue as equally serious.
- Leaving contradictions between the PO, drawing, sample and artwork unresolved.
- Assuming the inspector knows the buyer’s preferences.
- Reusing one generic checklist for unrelated products.
Before issuing the checklist, compare all references and resolve conflicts. An inspector should not have to decide whether the drawing, sample or email takes priority while standing in the factory.
Who Should Prepare the Inspection Checklist?
The buyer should define the product requirements, commercial priorities, tolerances, approved references and quality risks that matter to the order. Those decisions cannot be invented by the inspector.
The inspection company can help convert the buyer’s information into practical checkpoints, identify requirements that cannot be verified on site and point out missing methods, quantities or acceptance criteria.
The factory may provide useful technical information about its production process or available testing equipment. However, the buyer should approve the final requirements used for the inspection decision.
When Should the Checklist Be Finalized?
The checklist should be ready before the inspection date, with enough time to clarify missing references and confirm whether the necessary test equipment is available.
For a new or technically sensitive product, the important requirements should be defined before mass production starts. This allows the supplier, buyer and inspection team to work from the same standard instead of discovering an unclear tolerance after the order is finished.
Once the checklist is agreed, include its current version with the information provided before the visit. How to Prepare for a Pre-Shipment Inspection explains the other order and production information needed at that stage.
Frequently Asked Questions
How do you create a product inspection checklist?
Collect the current PO, specifications, drawings, approved references, artwork and packaging requirements. Convert each important requirement into a checkpoint that states the reference, inspection method, check quantity, acceptance criteria and required evidence. Remove duplicate or contradictory instructions before issuing the final version.
Who should prepare the inspection checklist?
The buyer should define the product and acceptance requirements. The inspection company can help turn those requirements into checks that can be performed at the factory. The inspector should not create new product standards or decide the buyer’s commercial preferences.
Is an approved sample enough for inspection?
No. An approved sample is useful for visual and construction comparison, but it does not replace written tolerances, test methods, component lists or packaging requirements. Objective specifications should be stated separately.
Should every inspection checkpoint use AQL?
No. AQL may be used to evaluate workmanship defects across a defined sample, while measurements, function checks, barcode scans, packaging tests and destructive tests may use different agreed quantities.
How detailed should an inspection checklist be?
It should contain enough information for a qualified inspector to repeat the check and reach a consistent result. If the method, reference or acceptance limit is still open to interpretation, the checkpoint needs more detail.
What information should an inspector record?
The record should show the samples checked, actual results, defects found, relevant photos, measurements, test conditions, barcode values where applicable and any limitation that affected the check.
Prepare the Checklist Before the Factory Visit
If you are preparing an inspection for an order in China, send us your product specifications, PO and key quality requirements. We can review the proposed scope, identify unclear checkpoints and confirm what should be prepared before arranging a Final Random Inspection.